Bogie Hearth Furnace Manufacturer Insights for Choosing a Reliable High-Temperature Processing Partner
2026-08-27
Every bogie hearth furnace looks capable on paper, but a reliable high-temperature processing partner is built on far more than wattage and chamber size. The difference shows up in ramp-rate consistency, load support after repeated cycles, and a manufacturer who understands your thermal profile instead of just quoting a standard model. In this preface, we skip the glossy specs and focus on the questions that matter before you sign a purchase order. Whether you're upgrading a heat-treat line or building a new ceramic firing process, these insights from THINKING-LONG can help you avoid the most common selection traps. For deeper guidance, explore THINKING-LONG.
How Leading Bogie Hearth Furnace Builders Handle Thermal Stress Without Cutting Corners
Thermal stress in a bogie hearth furnace isn't just a design parameter—it's the primary force that separates reliable equipment from constant maintenance headaches. Leading builders start by refusing to let insulation act as a mere liner. Instead, they interlock refractory modules with expansion gaps calculated from live load deflection data, not generic thermal expansion tables. The hearth car itself gets a floating deck system where individual castable blocks can shift independently under cyclic heating, preventing the hairline cracks that grow into structural failures. This approach means the furnace shell never sees the full brunt of differential movement.
Another practice that sets top-tier builders apart is how they manage the transition zones where the bogie meets the furnace body. Cheap designs rely on a single knife-edge seal that warps after a few months. Better builders use a dual-seal arrangement with a compressible ceramic fiber bulb that maintains contact even when the car sags slightly under load. They also route the heating elements away from these high-stress regions, using shaped radiant tubes that direct heat upward rather than blasting the seal faces directly. The result is a hot face that stays dimensionally stable without constant re-tightening of anchor bolts.
Finally, leading builders don't treat thermal stress as something to be solved only at the design stage. They instrument a handful of critical points—usually the hearth car perimeter and the crown arch—with thermocouples wired into a data logger that runs for the first hundred cycles. That data then feeds back into the refractory anchoring pattern, adjusting stud density where peak gradients actually occur rather than where a static FEA model predicted them. This closed-loop approach costs more upfront, but it eliminates the expensive post-installation patchwork that cheaper builders quietly fold into their service contracts.
Why Temperature Uniformity Often Reveals More Than a High Maximum Rating
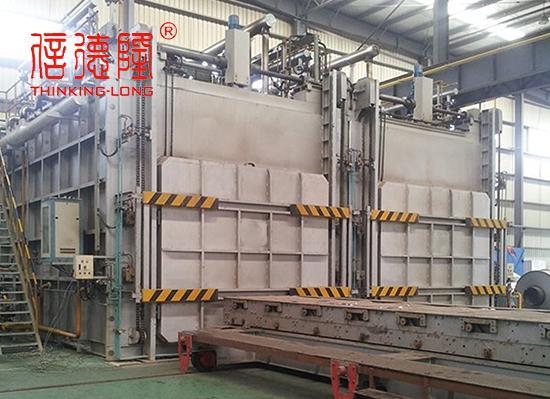
A furnace or kiln that boasts an impressive peak temperature can still deliver uneven results if heat distribution is poor. Uniformity measures how consistently heat reaches every corner of the chamber, which directly affects the quality of whatever you are firing or treating. A high maximum rating might look good on paper, but if the edges run hot while the center lags behind, you end up with warped parts, inconsistent finishes, or even material failure. In practice, most processes rarely operate at the extreme top of the temperature range; they rely on a stable, predictable environment across the entire working zone.
Think of it like baking a tray of cookies: an oven that can reach 300°C is useless if one side burns while the other stays raw. The same logic applies to industrial heat treatment, ceramics, or laboratory testing. Temperature uniformity ensures that every item experiences the same thermal history, which is critical for repeatability and meeting tight tolerances. Equipment with excellent uniformity often outperforms a higher-rated but poorly balanced alternative, because the real value lies in consistent, controlled conditions rather than an unused upper limit.
Another overlooked point is that chasing a higher maximum rating can sometimes compromise uniformity. To push the ceiling higher, manufacturers may use lighter insulation or stronger heating elements concentrated in one area, creating hot spots. In contrast, a well-designed system prioritizes even heat flow through careful element placement, airflow, and chamber geometry. When comparing options, ask for temperature mapping data across the working volume at your typical operating temperature—not just the maximum number on the spec sheet.
Reading Past the Spec Sheet: Frame, Lining, and Weld Details That Matter
A spec sheet will tell you the gauge of the steel and the overall dimensions, but it won't show how the frame corners are joined. Run your fingers along the inside edges where the front apron meets the side panels. If you feel a crisp, uniform seam with no sharp burrs or uneven gaps, that's usually a sign the manufacturer invested in proper fixturing rather than quick spot welds. On cheaper units, the metal tends to flex when you press on the center of the frame—something you'd never notice from a photo.
Lining gets even less attention. Many buyers assume a thicker coating automatically means better protection, but adhesion matters more than mil thickness. Look closely at the transition between the bowl and the flange. A quality lining should wrap smoothly around that curve without pooling, cracking, or showing a color shift. If the coating looks cloudy or you can scratch it with a fingernail in an inconspicuous spot, pass on it. That's a sign the surface wasn't prepped properly before application.
Weld details separate the pieces that last from the ones that fail in a couple of years. Inspect the underside if you can. A good weld will be consistent in width and have a slight crown, not a concave dip. You shouldn't see pinholes, spatter, or discoloration that extends far beyond the bead. These flaws often hide stress risers that eventually crack under daily use. The spec sheet won't mention weld penetration, but your eyes will.
Matching Furnace Capacity to Your Actual Workflow Instead of Buying Extra Volume
A bigger furnace doesn't automatically mean better output. It often just means more idle burners, longer heat-up times for half-loaded chambers, and a monthly energy bill that reflects space you never really use. Instead of sizing up as a safeguard, take a hard look at the batches you actually run week to week. If your typical load fills only sixty percent of the chamber, you're already paying for dead volume on every cycle.
Map out the real flow from incoming parts to finished heat treat. Count the baskets, racks, or fixtures that move through each shift—not the theoretical maximum. Many shops discover that a smaller, quicker furnace cycling more often keeps pace with production far better than a large unit sitting warm and waiting. The goal is to have the furnace working in rhythm with the rest of your floor, not creating a bottleneck downstream or upstream.
Also factor in how often you switch alloys, temperatures, or processes. A giant chamber is a liability when you need to change atmosphere or ramp profiles for a small specialty job. Matching capacity to your true workflow means less time purging empty space, tighter temperature control, and faster turnaround on the parts that actually keep your customers coming back. Skip the extra volume—tune the volume to the work.
What Ongoing Support Looks Like After the Installation Crew Leaves
Support doesn't vanish once the installation vans pull away. Most providers set up a direct line to a dedicated service team that already knows your layout. You can call or open a ticket through an online portal, and a technician who has access to your project notes will respond. This avoids repeating your history every time something minor comes up.
Many systems include remote diagnostics, so issues are often spotted before you even notice them. If a component drifts out of spec or a sensor reads oddly, you may get an alert or a scheduled check-in. Some providers also offer quarterly or annual maintenance visits that keep everything calibrated and catch wear before it turns into downtime.
Warranty coverage usually has clear terms: parts, labor, and response windows. You should receive a simple guide—not a thick binder—that explains who to contact and what to expect. If your needs change, good support will include options for upgrades, training refreshers, or reconfiguration without making you start from scratch.
Negotiating Performance Guarantees That Hold Up Under Real Production Loads
The first step is to stop accepting synthetic benchmarks as evidence. A vendor can make any number look good in a lab, but your production traffic has spikes, cold starts, and messy payloads that no controlled test will ever replicate. Insist on defining guarantees around your own workload profiles, captured over at least a full business cycle, not just a peak hour cherry-picked by the sales team.
Next, tie penalties to the moments that actually hurt your users. A 99.9% uptime SLA sounds impressive until you realize it still permits nearly nine hours of downtime a year, and often excludes the degraded states where pages load but features fail. Write the agreement so that breach is measured by end-to-end latency percentiles and error budgets on real user sessions, not by server ping responses.
Finally, make the remediation path explicit before you sign. If performance drops under load, you need to know who pays for the extra capacity, how quickly the vendor must escalate, and what evidence they must provide to prove the fix. Without that operational detail, a performance guarantee is just marketing copy wearing a legal costume.
FAQ
Focus on the hearth car seal arrangement and the way the furnace floor interfaces with the car deck. A continuous flat seal with pneumatic or mechanical clamping that remains effective through repeated thermal expansion will outlast simple sand seals. Also check that the hearth car wheels, rails, and drive chain are sized for the maximum load plus thermal growth, not just the nominal charge weight.
Ask for references where the furnace runs the same temperature range you need, not just the same industry. A builder with deep experience in 1100°C cycling will have different element anchoring and insulation retention methods than one focused on 700°C aging. Request a walk-through of a furnace that has been in service for at least five years and observe whether the lining shows excessive cracking or spalling near the burner or element openings.
Instead of asking if the door seals well, ask how the seal behaves after the furnace has been hot for eight hours and then cooled for a shift. Whether they use a knife edge, ceramic fiber gasket, or pneumatic compression, you want to know what replacement intervals they recommend and whether the sealing surface can be adjusted without a full rebuild. Also ask if the door can be opened partially for unloading without losing the entire atmosphere, if that matters for your process.
The control panel gets all the attention because it is visible, but a bogie hearth furnace lives or dies by how reliably the loaded car moves in and out under load. If the drive chain, pinion, or cable system is undersized, a fully loaded car can jam or creep, causing misalignment and seal damage. Look for a drive with overload protection, manual override, and positioning feedback that does not rely on limit switches alone. A cheap PLC can be upgraded later; a weak drive system cannot.
Give them a real thermal profile with ramp rates, soak times, and load configuration, then ask them to calculate the required heating input and fan circulation pattern. If they come back with only a quote and no thermal calculation, they are likely copying a standard design. A manufacturer who understands your process will ask about part spacing, allowable temperature uniformity, and atmosphere control before proposing burner or element layout.
Watch for vague phrases like 'high-quality insulation' without specifying the ceramic fiber grade, density, and anchoring method. A proposal that lists only total kW without breaking down element type, watt density, and spacing is often hiding an undersized heating system. Also be suspicious if the furnace shell is thinner than 6 mm on a high-temperature unit or if the hearth car deck uses a single layer of castable instead of a composite with expansion joints.
Ask each builder to provide the calculated heat loss at your operating temperature, including wall, hearth, door, and flue losses, not just an overall percentage. Compare the insulation stack thickness and the type of low thermal mass materials used. A furnace with a smaller gross kW rating can still waste more energy if it has poor door sealing or a heavy hearth car that must be reheated after every cycle. Insist on seeing the thermal model, then follow up with a reference customer about actual gas or electric consumption per load.
Conclusion
When selecting a bogie hearth furnace, the difference between a dependable partner and a costly mistake often hides in details that never appear on a glossy datasheet. Leading builders treat thermal stress as a structural engineering challenge, not just a matter of thicker steel. They design frames with controlled expansion zones, use anchoring systems that let the refractory lining breathe without cracking, and weld seams in sequences that minimize distortion during cycling. Temperature uniformity, rather than a headline maximum rating, becomes the true test of value: a chamber that holds ±5°C across the load at 1100°C will outperform one that spikes to 1200°C but drifts by 40°C. That demands careful burner placement, airflow modeling, and sometimes sacrificial baffles that can be replaced as they wear. Reading past the spec sheet means inspecting corner joints, insulation density, and door seal quality—details that reveal how the furnace will behave after a thousand cycles, not just on day one.
Equally important is sizing the furnace to your actual workflow. Many buyers end up paying for extra volume they never use, while struggling with long heat-up times and energy waste. A good manufacturer asks about your batch sizes, loading patterns, and future growth before recommending chamber dimensions. After installation, support should extend beyond a phone number: look for partners who offer remote diagnostics, scheduled thermal surveys, and quick access to replacement heating elements. Finally, performance guarantees need to be negotiated against realistic production loads, not empty chambers. Specify acceptable temperature spread under a full load of your typical parts, and define how deviations will be measured and corrected. A reliable partner will put those numbers in writing and stand behind them—the clearest sign you are working with a manufacturer that understands the long-term cost of high-temperature processing.
Contact Us
Contact Person: Qian Xijun
Email: [email protected]
Tel/WhatsApp: 8613961736750
Website: https://www.thinkinglong.com/