Shearing Machine Manufacturer: How Leading Brands Ensure Precision and Durability
2026-10-22
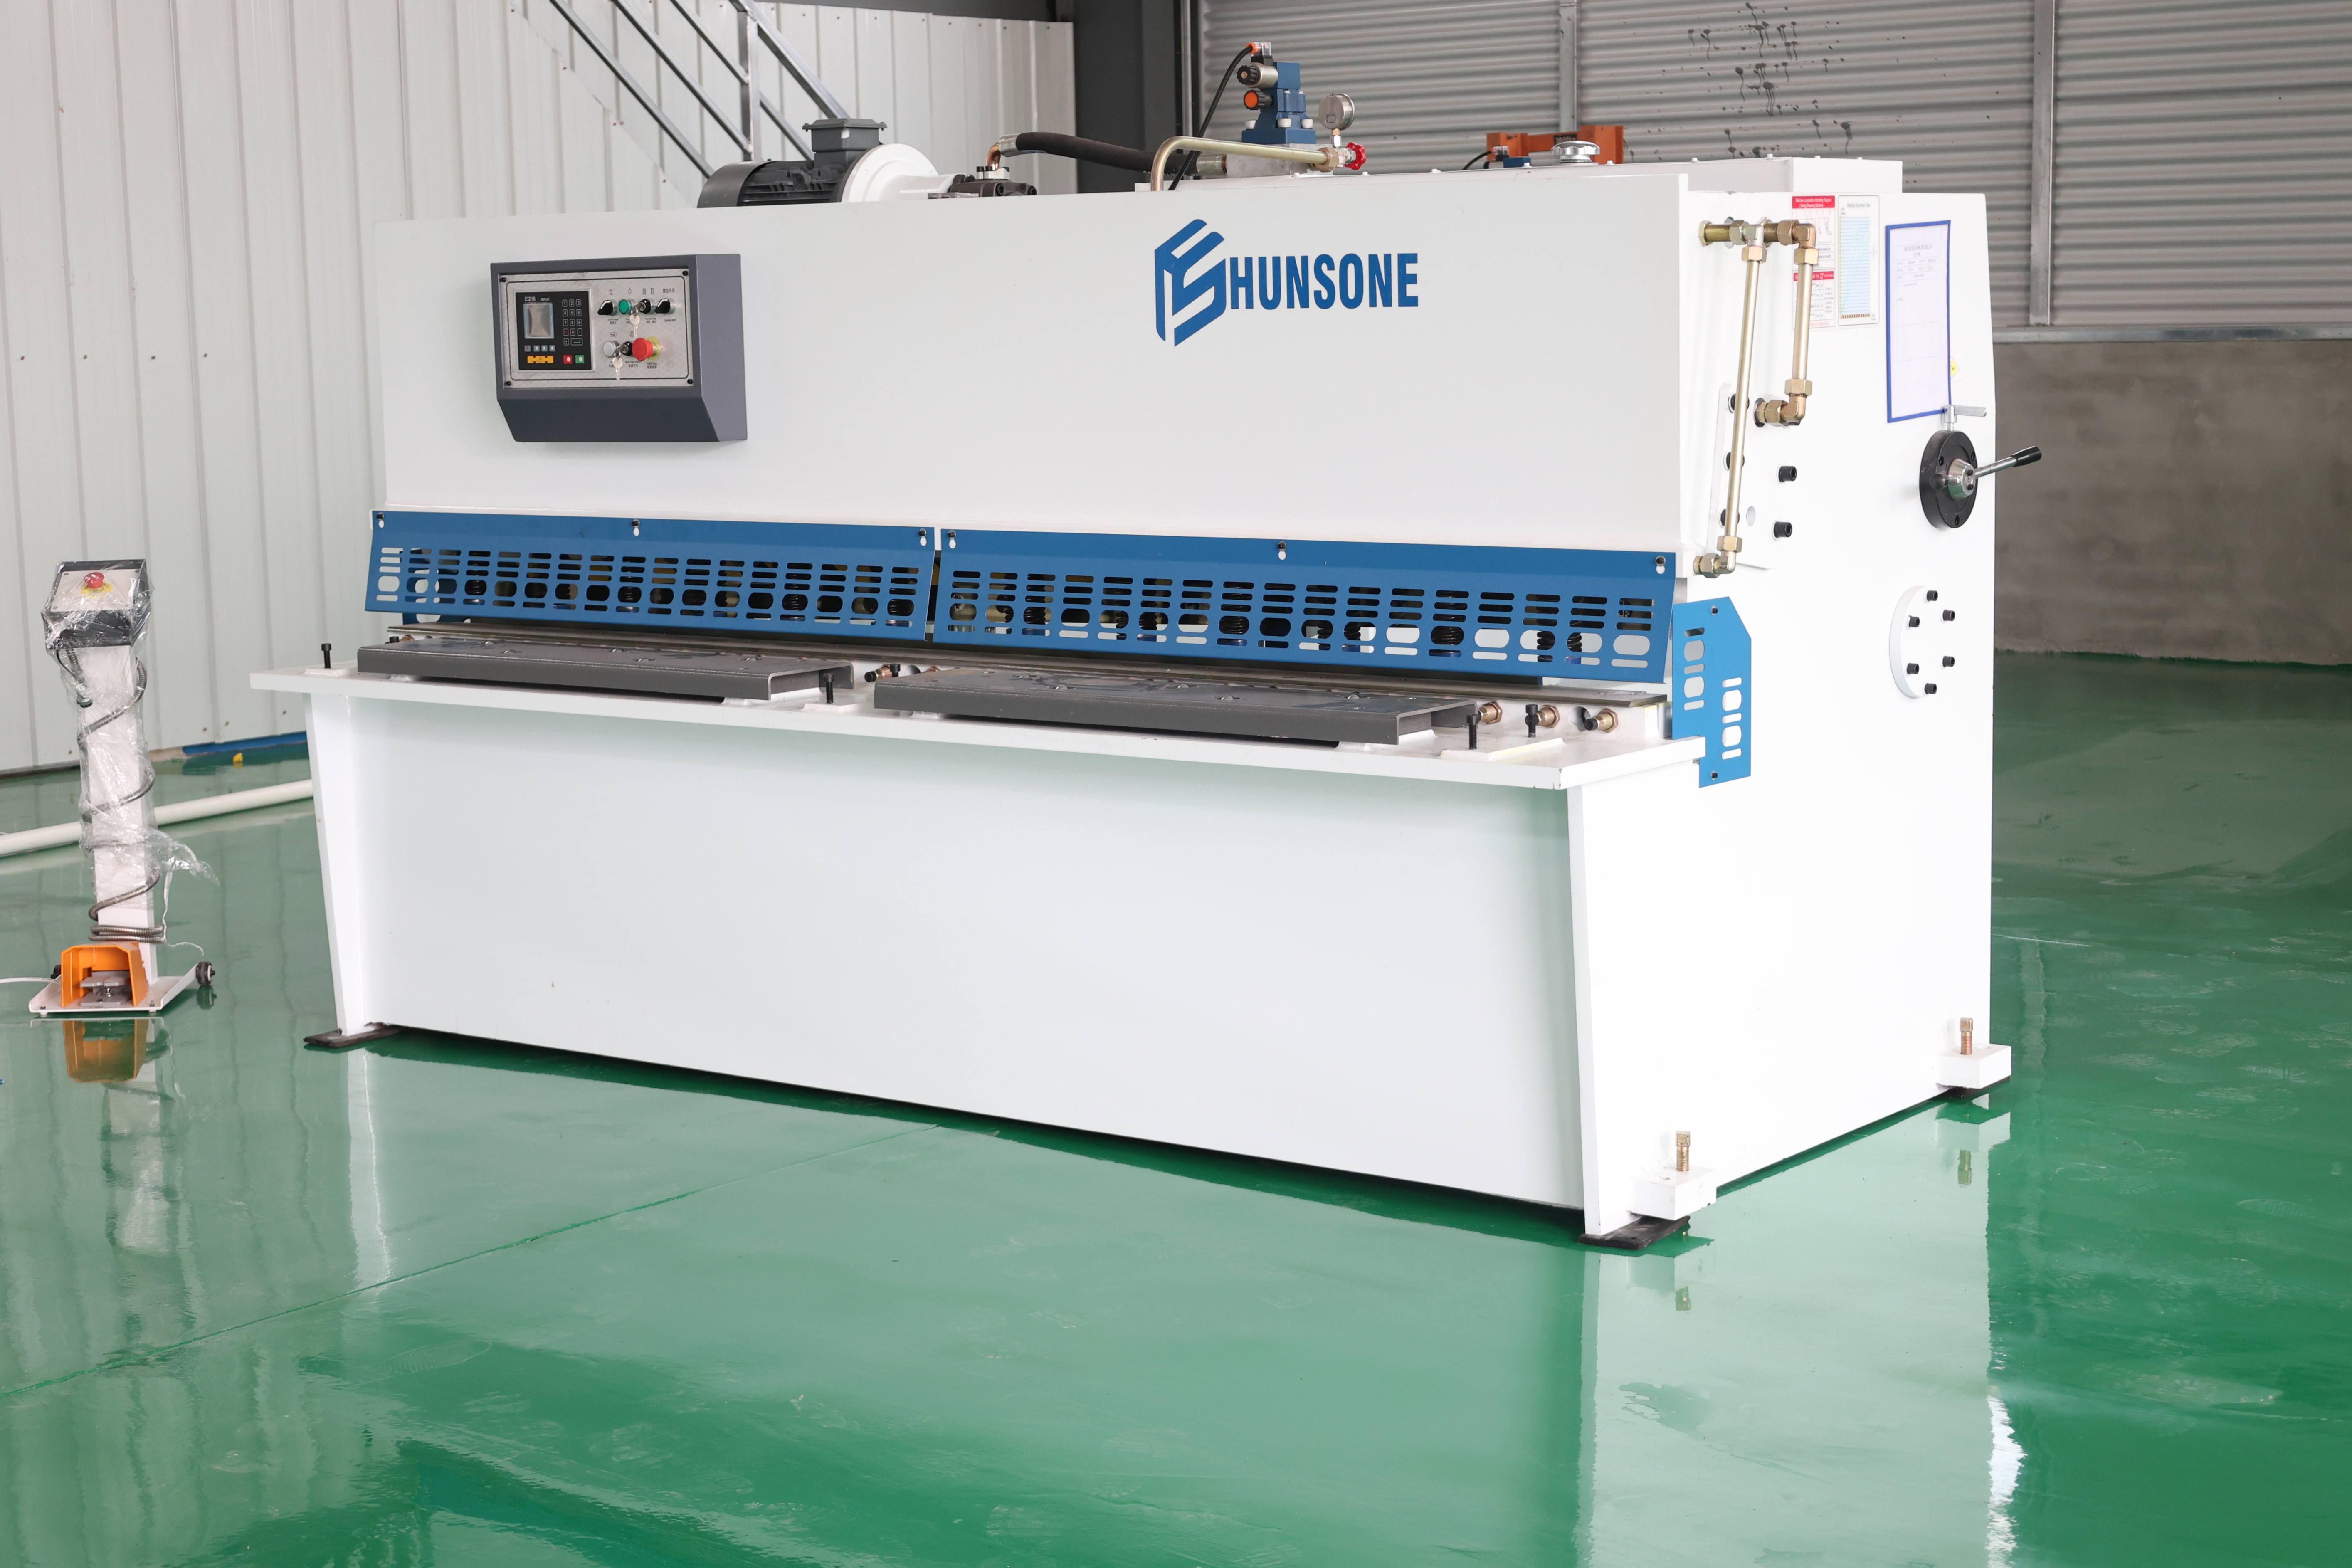
A shearing machine is only as good as the cut it makes after five years of daily use—most buyers learn that the hard way. Precision and durability don't come from marketing claims; they come from how a manufacturer handles frame construction, blade clearance, and the small tolerances that show up only after thousands of cycles. That's where leading names earn their reputation. In this article, we break down the design and production decisions behind reliable shearing machines, using HUNSONE to illustrate what to look for before you invest.
The Metallurgy Behind Long-Lasting Blades
Blade longevity starts with alloy selection, but the real story is in the balance between hardness and toughness. Steels with higher carbon content, like 1095 or Aogami Super, form more iron carbides during heat treatment, which resist abrasive wear. Yet too much carbon makes the edge brittle. Makers compensate by adding elements such as vanadium or tungsten, which create exceptionally hard, fine-grained carbides that hold an edge without sacrificing the blade’s ability to flex under lateral stress.
Heat treatment often matters more than the raw steel composition. A precise austenitizing soak followed by a fast quench locks in a fine martensitic structure, while multiple tempering cycles relieve internal stress and convert some retained austenite. Some workshops push further with cryogenic treatment—cooling the blade below -100°F—to transform leftover austenite into martensite. That extra step refines the grain and can lift edge retention by a noticeable margin, though the exact gain depends on the alloy and the quench speed achieved beforehand.
How Precision Alignment Is Achieved—and Tested
Achieving precision alignment starts with a stable mechanical foundation and high-resolution motion stages—typically piezo-driven or crossed-roller bearing designs—that can move in increments far smaller than a micron. Feedback from capacitive sensors or laser interferometers feeds a closed-loop controller, which compares the actual position of the component against a commanded target and issues corrections in real time. Instead of relying on a single “perfect” adjustment, skilled technicians often work through a sequence of coarse-to-fine moves: first rough positioning to bring the part within the capture range of fine sensors, then iterative nudges that converge on the target. This approach avoids overshoot and minimizes the influence of backlash or thermal drift between moves.
Testing alignment accuracy demands more than a single pass/fail check. A common practice is to use an autocollimator or a laser interferometer to measure angular and translational errors relative to a well-characterized reference surface, such as an optical flat or a precision-ground granite rail. Multiple measurements are taken after deliberately disturbing the system—loosening and retightening a clamp, cycling the stage, or waiting for thermal equilibrium—to confirm that the alignment returns to within tolerance. Long-dwell tests in a temperature-controlled enclosure reveal slow creep caused by adhesive settling or residual stress in machined parts, which might otherwise pass a quick verification but drift out of spec hours later.
The final proof often comes from functional performance under load: an optical system is checked for wavefront error or spot symmetry, a linear rail for straightness over its full travel, and a spindle for radial runout at speed. Because every measurement chain has its own uncertainty, alignments are cross-checked with two independent methods—for instance, a dial indicator and a laser displacement sensor—and the results must agree within a few tenths of a micron before the setup is released. This layered verification catches tooling errors, sensor miscalibration, and hidden flexure that a single instrument could miss.
Heat Treatment Practices That Prevent Premature Wear
Effective case hardening starts with matching carbon potential to part geometry, not just aiming for a deep case. Pushing carburizing temperatures too high or holding parts too long creates networks of grain-boundary carbides that crack and spall under contact stress, which accelerates wear instead of slowing it down. A better practice is to keep the carbon potential between 0.8% and 0.9% during the boost phase and then drop it for diffusion, producing a tough martensitic case without brittle carbide films. For nitrided components, controlling the white layer thickness is equally important: a thin, dense compound layer resists scuffing, while a porous, overly thick one flakes away.
Tempering deserves more attention than a single lookup on a hardness chart. Alloy steels like 4340 or 52100 often respond best to a double temper, with the first cycle removing most of the as-quenched stress and the second catching any retained austenite that transformed during cooling. Skipping the second temper leaves unstable microstructure that shifts in service, changing clearance and creating localized wear hotspots. Also avoid the temper embrittlement range around 250–400°C for many chromium and manganese steels; staying below or above that window keeps impact toughness high enough to absorb occasional overloads without surface cracking.
Cryogenic treatment between quenching and tempering is not a gimmick when retained austenite is an issue. In high-carbon tool steels and case-hardened gears, even 10–15% retained austenite can soften the surface and lower rolling contact fatigue life. Cooling to -80°C or lower converts much of that austenite to martensite, after which a light temper restores a few points of toughness. The result is a harder, more stable surface that resists micropitting and delamination wear better than quench-and-temper alone.
Stress Testing Beyond What the Manual Requires
Most manuals stop at nominal load, room temperature, and steady-state conditions. That leaves a blind spot where real failures live. I’ve watched a power rail pass every factory test, then collapse under a 20 ms brownout with a hot chassis and all peripherals drawing peak current at once. Manuals rarely stack those conditions because they weren’t written for field chaos.
One approach we use is to pick apart the assumption list in the spec and deliberately break two or three at the same time. If the derating curve says 80% load at 60°C, we’ll run 95% load at 65°C with airflow partially blocked. If the watchdog timeout is 500 ms, we’ll inject resets at 490 ms while the firmware is mid-write to flash. The goal isn’t to prove the design wrong; it’s to map where the margin actually ends.
We keep a separate notebook for results that fall outside the official pass/fail criteria. Those numbers — how long a capacitor survives ripple above rating, how many hot-plug events a connector takes before contact resistance climbs — become our own derating rules. It’s the difference between shipping a product that meets the datasheet and shipping one that survives the user’s worst Tuesday.
Calibration Routines on the Factory Floor
On many factory floors, calibration isn't a quarterly event tucked into a binder. It's folded into shift start, after tool changes, or whenever a machine throws a reading that doesn't match the part in hand. A machinist might run a quick check with a known test block before trusting a micrometer on a final inspection. Those routines stick because they solve immediate problems: a dial indicator that drifts after lunch can scrap a whole tray of housings. So the floor develops its own rhythm—check the master, note the offset, sign the log.
Then there's the environmental side. Temperature swings near loading doors or vibrations from a stamping press can push a coordinate measuring machine out of spec by mid-morning. Some teams place a reference part on the CMM fixture every two hours and watch the delta. If it creeps past a few microns, they pause and rerun the compensation routine instead of chasing phantom dimensional errors later. That kind of in-process verification often matters more than the annual calibration sticker on the side of the machine.
Documentation tends to be lighter than the quality manual suggests. A whiteboard next to a torque wrench station might list the last verified value and the date, with initials. No fancy software. But the practice is alive because the people running the line know that a tool out of calibration isn't a paperwork problem; it's a bad batch waiting to happen. That shared understanding keeps the routines from becoming empty rituals.
Feedback Loops That Shape Each New Generation
Children don’t simply absorb the world around them—they push back, reinterpret, and remix what they receive. A parent’s habits around technology become raw material for a teenager’s own rituals, which then drift further as friends and recommendation systems amplify certain choices. That back-and-forth isn’t a flaw; it’s the mechanism. Each small adjustment a young person makes feeds into the environment the next cohort inherits.
Music taste offers a clear example. A generation raised on streaming playlists learns to treat songs as modular pieces, not albums. The platforms notice skipping patterns and tweak suggestions, which trains listeners to expect even more immediacy. By the time those listeners become parents, their nostalgia and ambient listening shape what their own kids consider “normal,” and the cycle tightens again.
Schools mirror the same loop. Teachers adapt to students’ shortened attention spans by shortening lessons, which normalizes brevity, which then gets reported back as a learning style. None of this is neutral—every turn rewards certain skills and lets others atrophy. The real question isn’t whether these loops exist, but who gets to pull the levers inside them.
FAQ
Leading brands often rely on high-grade alloy steels for blades and frames, then subject them to heat treatment processes like induction hardening. This creates a hard outer surface while retaining a tough core, so the machine holds its edge and resists deformation over years of heavy use.
They run a series of controlled cutting trials on different sheet thicknesses and materials. Each cut is checked for straightness, edge finish, and dimensional accuracy. Only machines that meet tight tolerance bands are cleared for shipment.
It usually comes down to frame rigidity and the way components are aligned during assembly. Premium manufacturers use stress-relieved welded structures and precision-machined bearing surfaces, which prevent the frame from flexing or shifting under load.
Blade clearance must be adjusted to match the material thickness and tensile strength. If it is too wide, the material bends and tears; too narrow, the blades wear quickly. Reputable manufacturers provide clear adjustment mechanisms and even motorized systems for repeatable settings.
Many integrate cooling or lubrication systems directly into the cutting zone. This keeps blade temperature stable, reduces thermal expansion, and flushes away debris, all of which help preserve both precision and blade life.
Check the machine's throat depth, frame construction, and the type of gibs or guides used. Forged or cast components with hand-scraped surfaces indicate careful fitting. Also ask about the warranty on the frame and cutting beam, as longer coverage often reflects confidence in durability.
Yes, some manufacturers now use finite element analysis to optimize the frame shape, removing unnecessary weight while adding stiffness where it counts. Others use hydraulic systems with proportional valves for smoother, more controlled blade movement, which reduces shock loads on the whole structure.
Even the best machine will drift if blades are not sharpened or replaced on schedule, and if guideways are not kept clean and lubricated. Leading manufacturers often provide detailed maintenance logs and quick-access panels to make these tasks easier, helping owners keep the machine within its original tolerances.
Conclusion
Precision and longevity in shearing machines don't come from marketing claims—they start deep in the metallurgy of the blades. Leading manufacturers select high-alloy tool steels with carefully controlled carbide distribution, then refine edge geometry and hardness through iterative heat treatment. This isn't a one-size-fits-all soak-and-quench. They adjust austenitizing temperatures, quenching media, and tempering cycles to match each blade's cross-section and intended workload, so the cutting edge resists chipping and deformation far beyond standard expectations. On the assembly floor, precision alignment is treated as a measurable discipline rather than a best effort. Laser interferometry and dial indicators verify ram-to-bed parallelism within microns, while blade clearance is set and rechecked under simulated cutting loads. No machine leaves the line without passing a stress test that deliberately exceeds the manual's rated capacity, including cycling at maximum tonnage, off-center loading, and rapid stroke rates to expose any latent weakness.
What really separates top-tier builders is their refusal to rely on final inspection alone. Calibration routines are embedded into daily production, not just scheduled maintenance—technicians check backgauge accuracy, blade gap, and hydraulic pressure every shift, logging the data for trend analysis. When a deviation appears, it triggers adjustment before a part can drift out of tolerance. Then there's the often-overlooked feedback loop: after machines reach customer sites, manufacturers collect wear patterns, maintenance logs, and operator observations. That field data feeds directly into the next generation, prompting changes in blade metallurgy, guideway design, or control software. Over time, this loop tightens tolerances and extends service life in ways that a static design never could. The result is a shearing machine that doesn't just pass a spec sheet on day one—it holds that precision after years of daily cuts.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/